




Contents
- Which machine is needed to cut Plexiglas?
- What precision can be expected from laser cutting?
- What budget should be planned for a laser cutter?
- What should be checked before buying in France?
- Frequently asked questions
Choosing a CO₂ laser cutting machine for Plexiglas depends on three essential criteria: the type of laser source, the power required based on the thickness of the Plexiglas to be cut, and the overall budget for the laser cutting setup. This article compares CO₂ lasers with diode lasers, as well as the saw and CNC router. It also details the edge quality to expect, prices in euros, and the checks to carry out in France before purchase.
Which machine is needed to cut Plexiglas?
Plexiglas belongs to the PMMA family, also known as acrylic glass. Not all laser sources process it the same way. The difference depends on the wavelength, then on the power and bed size: these three criteria should be compared separately.
Clear acrylic, diode, fiber and CO₂ source
For cutting Plexiglas, a CO₂ laser machine is particularly well suited to transparent sheets. Conversely, the beam of a blue diode laser generally passes through clear acrylic without managing to cut it. A diode can, however, be used to cut certain opaque and dark types of acrylic. As for fiber lasers, they can act on the reflective layer of mirrored acrylic, but they are not a versatile solution for cutting PMMA.
Thermoflan offers flatbed CO₂ laser machines suited to cutting Plexiglas sheets. Within this range, the glass CO₂ laser tube is an economical solution for routine cutting and engraving work. The RF (radio frequency) tube, meanwhile, provides a finer and more stable beam, which is particularly useful for producing precise outlines and cuts requiring great finesse.
The choice of laser source therefore plays an essential role in the quality and precision of laser cutting and engraving of Plexiglas, as well as in the results obtained when engraving Plexiglas.
What power is needed based on thickness?
The power of the CO₂ laser tube is a key factor in determining the thickness of Plexiglas that can be cut. For laser cutting acrylic, a 40 to 60 W source generally cuts sheets 5 to 6 mm thick. With 80 W, laser cutting can reach 8 to 10 mm in a single pass. CO₂ laser tubes of 150 to 200 W can cut Plexiglas and PMMA sheets 15 to 20 mm thick. For laser cutting thick Plexiglas, from 20 mm of PMMA upward, CO₂ laser machine configurations may require a power between 200 and 650 W. Some laser cutting machines even advertise a cutting capacity of up to 30 mm of Plexiglas.
These laser cutting capacities for Plexiglas are indicative only. The maximum cuttable thickness, cutting speed and finish quality depend on the laser machine used, the power and speed settings, and the characteristics of the acrylic sheet. At greater thicknesses, focal point adjustment, compressed air assist and fume extraction require particular attention. The rule of thumb of 10 W per millimeter of acrylic thickness is a useful starting point for choosing the power of a CO₂ laser machine, but it does not allow precise calculation of cutting time. For comparable material and cutting parameters, a higher CO₂ laser power generally allows cutting thicker Plexiglas sheets or increasing cutting speed.
| CO₂ power | Indicative acrylic thickness | Note |
| 40 to 60 W | Up to 5 to 6 mm | Indicative value |
| 80 W | 8 to 10 mm | In a single pass |
| 150 to 200 W | 15 to 20 mm | Speed and finish not guaranteed |
| 200 to 650 W | From 20 mm | Focus, air and extraction to monitor |
Working area and sheet passage
The working area of a CO₂ laser cutting machine is chosen according to the size of the Plexiglas sheets and the dimensions of the parts to be cut, regardless of the laser tube power. The working sizes offered in Thermoflan’s CO₂ range range from 450 × 300 mm to 1,600 × 1,000 mm, to meet different cutting and laser engraving needs.
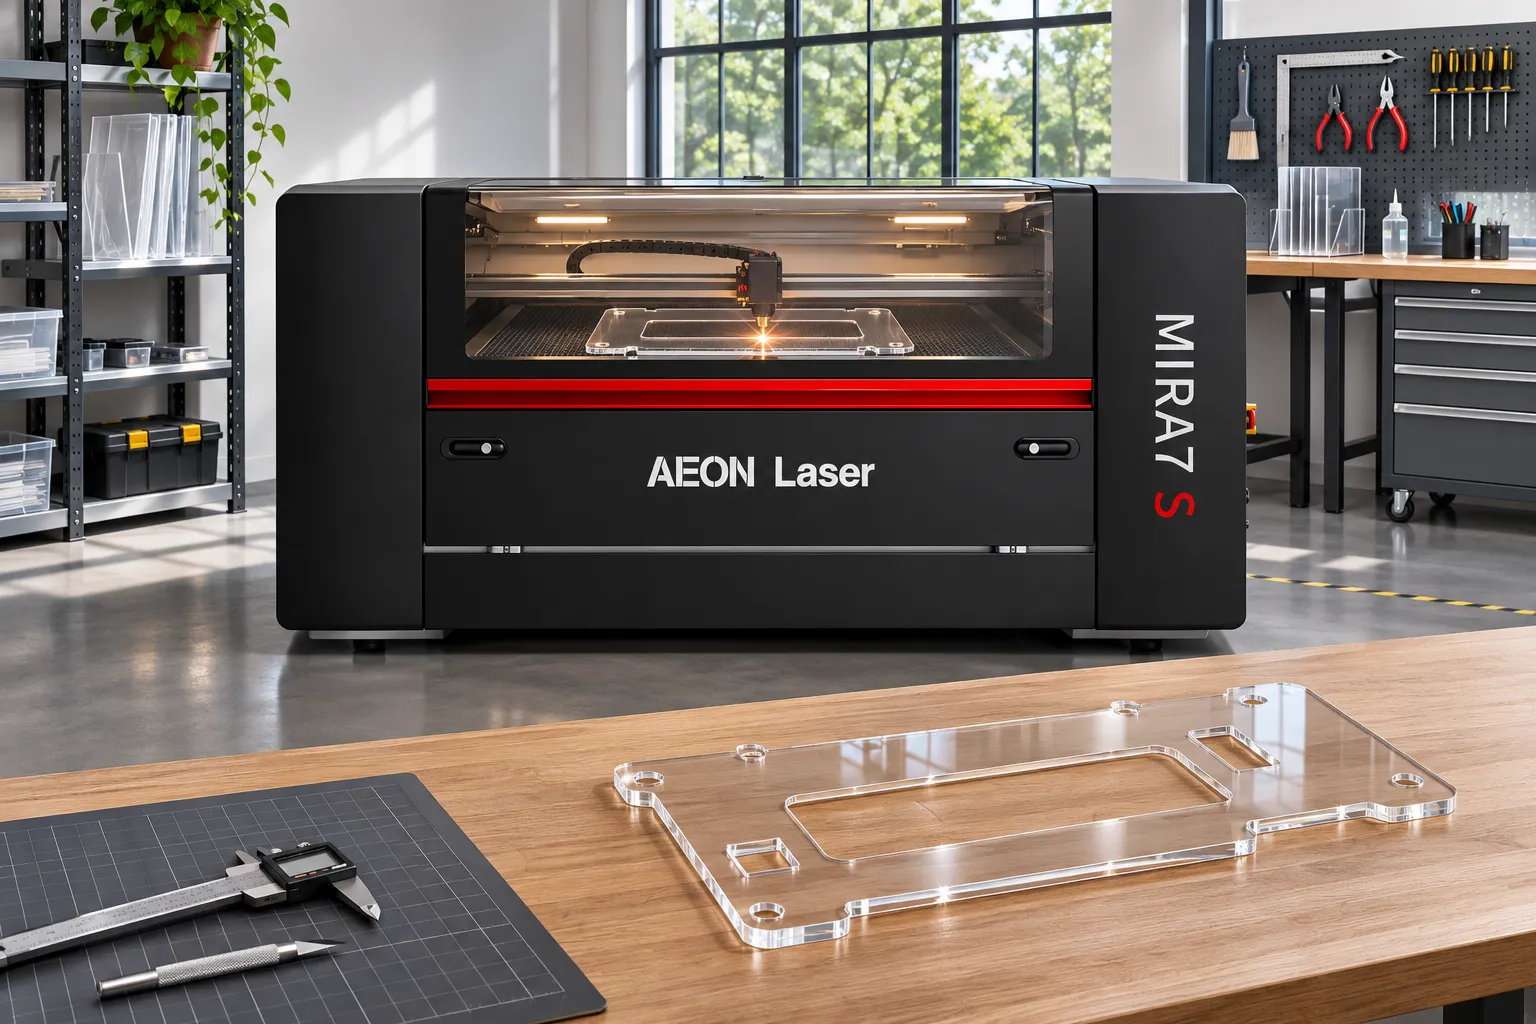
The Redline Mira 7 S, for example, has a working area of 700 × 500 mm and pass-through doors at the front and back of the machine. These openings allow working on parts longer than the cutting bed while keeping the same passage width.
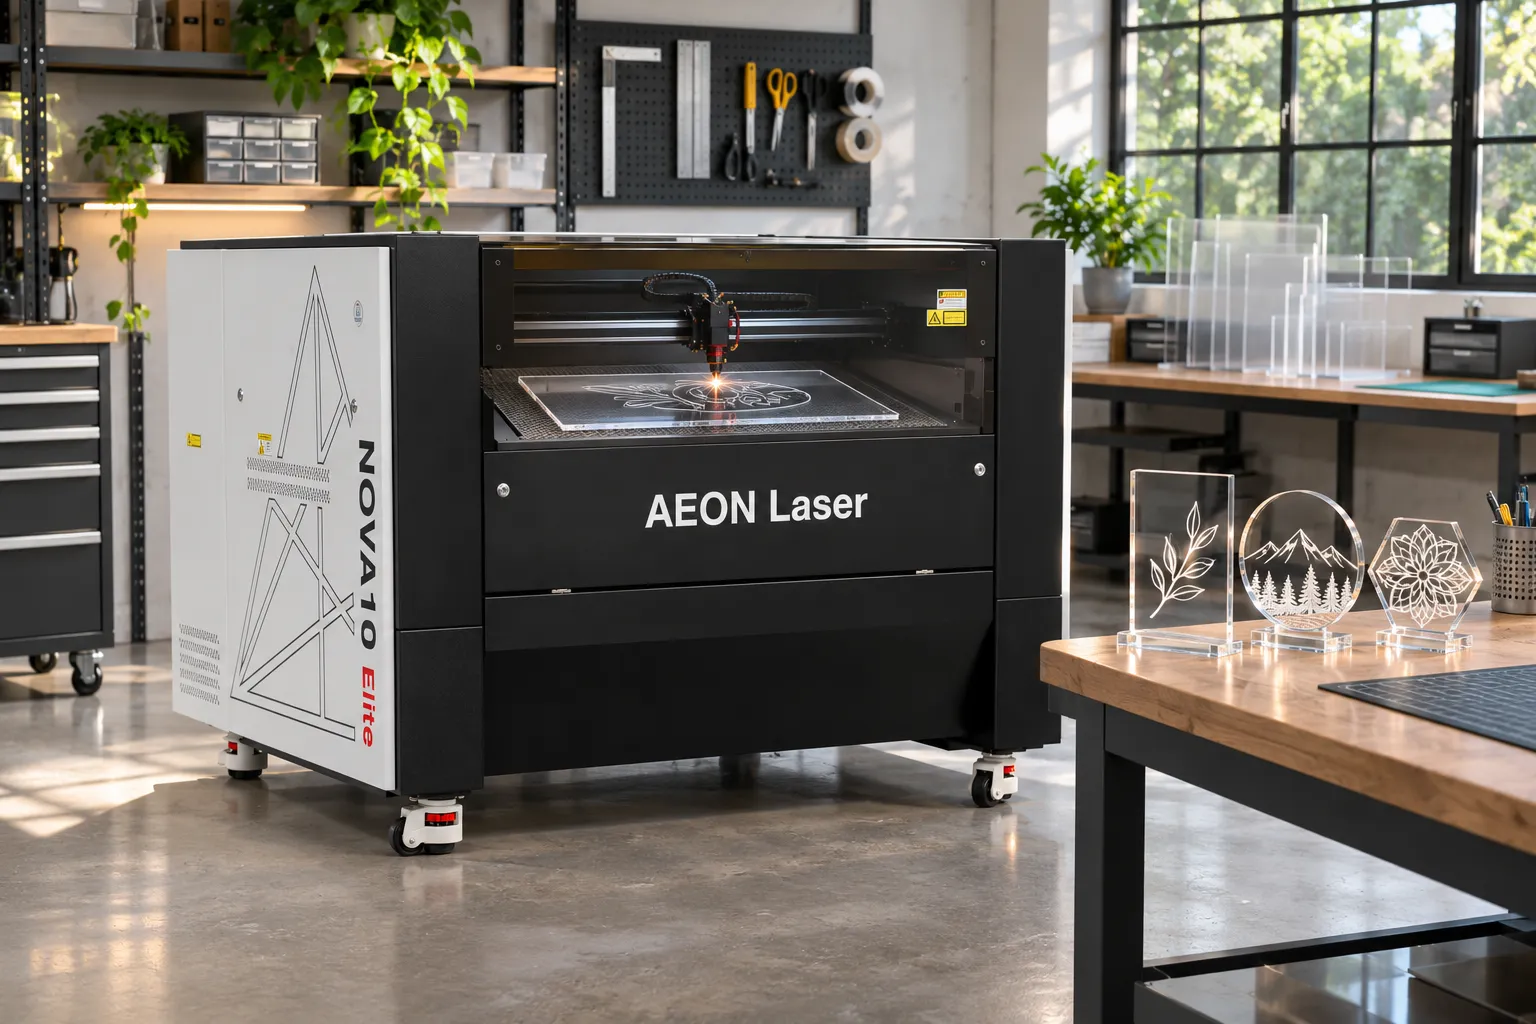
Other CO₂ laser machines meet specific needs: the compact Mira 5 is suited to prototyping and small runs; the Nova Elite 14 allows working on large cutting areas; while the I4000 has a large work table equipped with four pass-through doors.
In practice, before choosing a laser machine to cut acrylic, it is important to measure the dimensions of the longest and widest sheets to be processed. These measurements help determine whether a large working area is needed or whether a machine with pass-through doors meets production requirements.
Tip
Choose the laser source based on your acrylic sheet
Not all laser sources process PMMA in the same way. First identify the type of sheet (clear, colored, mirror) and its thickness, then check that the chosen source and power are suitable.
How precise can laser cutting be?
Once the machine is sized, the result is judged on the part itself. Laser cutting leaves an edge whose appearance, kerf width and quality vary depending on the sheet and settings. The type of PMMA, cast or extruded, and coated sheets such as mirror acrylic also affect the result.
Edge of an acrylic sheet
The heat of a CO₂ laser can leave a glossy edge on an acrylic sheet without sanding. A slight burr may nevertheless appear on the top and bottom faces. The kerf, i.e. the width of material removed, also increases with thickness:
- 3 mm sheet: kerf of approximately 0.26 to 0.44 mm depending on cutting conditions.
- 10 mm sheet: kerf of approximately 0.64 to 0.82 mm depending on cutting conditions.
- Feed too slow: the edge may become matte.
- Feed too fast: grooves may form on the edge.
Beyond speed, focus, air assist and extraction also influence the finish. Adjust them on an offcut of the same reference before judging an edge.
Cast and extruded PMMA, engraving and durability
Cast PMMA, sold under the GS reference, generally gives a white, high-contrast frosted laser engraving. Conversely, extruded XT produces a less contrasted engraving. On a clear sheet, engraving on the back can be tested in addition to engraving on the front face.
These two families also differ in sheet consistency. Material documentation gives thickness tolerances of approximately ±15% for cast and ±5% for extruded. These are sheet tolerances, not cutting tolerances.
Once the part is cut, stresses near the laser edge can cause cracking after bonding. Annealing is then recommended, to be validated depending on the part: 80 °C for GS and 70 to 80 °C for XT. In both cases, it lasts at least 2 h.
The case of mirror acrylic
Mirror acrylic is a PMMA sheet with a reflective coating. It thus differs from clear acrylic sheet without coating, but also from a glass mirror. For laser cutting of mirror acrylic, the described process consists of engraving on the back of the sheet, followed by CO₂ laser cutting. It is important to monitor the heating of the material and the condition of the reflective coating after each test cut.
As with clear acrylic sheets, obtaining a glossy edge guarantees neither dimensional compliance nor straightness of the cut part. The pigmentation of the PMMA and the sheet thickness can also influence the final appearance after laser cutting.
What budget should be planned for a laser cutter?
The purchase price of a CO₂ laser cutting machine depends mainly on the laser source and its power, but it represents only part of the total cost of the cutting station. The figures below give orders of magnitude in euros for the French market. They also make it possible to compare the cost of laser cutting with other solutions, such as a saw or a CNC milling machine.
Displayed prices and comparable configurations
On the French market, a 40 W diode laser costs around €1,799 for engraving on PMMA only. A 40 W CO₂ laser starts at around €5,800, while an 80 W CO₂ laser machine costs about €8,000. These different laser configurations are not, however, directly comparable quotes, as they rely on different technologies and equipment.
At Thermoflan, the Redline Mira 7 S CO₂ laser machine starts at €7,750 excl. VAT.
The Redline Mira 7 S laser cutting machine is available with several power configurations: a 60 W, 80 W or 90 W Premium glass CO₂ laser tube, or a 30 W or 60 W RF laser tube. These different sources and powers are detailed on the Redline Mira 7 S laser page. To compare laser cutting machine prices properly, it is therefore important to always specify the type of laser source and the tube power.
Total cost of the complete setup
A comparable budget includes the machine, the table, the focusing and plate handling. It also covers extraction or filtration, compressed air, software, installation and training. Be sure to ask suppliers for a detailed quote based on this same scope.
Operation then adds maintenance, energy, consumables, material losses, operator time and any finishing. An RF tube generally lasts longer than a glass tube, but replacing a glass tube usually costs less. In practice, economic throughput is measured in accepted parts per hour, after loading, inspection, cleaning and scrap, not by the machine datasheet speed alone.
Saw, CNC router and finishing cost
CO₂ laser cutting is contactless and produces no chips, including for contours and internal cutouts. A CNC router, by contrast, requires clamping the sheet and removing chips. However, it allows drilling and depth-controlled pockets, and its budget shifts to the cutter, clamping, extraction and edge finishing.
A saw fitted with a blade suited to PMMA is mainly suitable for repeated straight cuts. Its edge may require finishing when optical appearance matters, and this finishing time then adds to the cost per part.
What to check before buying in France?
A price and a datasheet are not enough to validate a machine. Secure the purchase by testing on your own sheets, sizing the extraction correctly and checking the compliance documents required in France.
Test on the planned sheets
The purchase test piece uses the exact references of the GS or XT sheets, with their colours, films and thicknesses. Its layout includes a straight line, an angle, a small hole, an internal contour and a laser engraving area. Before the test, set the acceptance criteria:
- Dimensions and edges: dimensional tolerances and acceptable appearance of both faces.
- Engraving and defects: expected contrast, acceptable marks and burrs.
- Production: cycle time and acceptable scrap rate.
The test is carried out on the proposed machine, at the maximum planned thickness, with the intended extraction and accessories. Keep the parameters and photographs, then repeat the cut to verify that precision remains consistent.
Extraction, emissions and fire
According to measurements published by INRS in December 2014, laser cutting of PMMA releases 200 to 300 mg/m³ of methyl methacrylate at 30 cm from the point of impact. The same measurements found 0.5 mg/m³ of formaldehyde, which does not represent individual exposure over 8 hours. For comparison, INRS gives a French occupational exposure limit value (VLEP) of 205 mg/m³ over 8 hours and 410 mg/m³ short-term for methyl methacrylate.
Where emissions cannot be eliminated, articles R. 4222-12 and R. 4222-13 of the Labour Code require their capture as close to the source as possible. A cutting job must also not be left unattended. Check the extraction and safety interlocks before starting, then clean the bed, nozzles, optics and air passages according to the manual, as this cleaning limits the build-up of flammable residues.
Compliance and acceptance of the workstation
Before purchase, check the manual, the CE marking, the declaration of conformity and the interlocks. Also verify the laser class in the configuration actually used and the extraction requirements. A Class 1 rating alone does not tell you anything about fumes or fire risk.
Workstation risks are listed in the single risk assessment document required by article R. 4121-1 of the Labour Code. If the documentation does not rule out the optical risk, article R. 4452-7 provides for calculation and measurement of exposure where necessary. Acceptance ultimately covers the complete workstation, its safety devices, its extraction and training. The standards NF EN 60825-1 and NF EN ISO 11553-1 serve as references for reviewing the file. The ISO 11553-1:2020 edition replaced the 2005 edition in April 2020.
CO₂ Lasers for Plexiglass Cutting
Working area, power based on thickness, test on your sheets: Thermoflan experts help you size your laser cutting station.

Frequently Asked Questions
What is the best tool for cutting plexiglass?
A CO₂ laser cuts PMMA without mechanical stress or chip production, and it handles contours, internal cutouts and engraving. By contrast, a milled edge can be matte or satin depending on the machine, the cutter and the speed, and then flame-polished. The abrasive disc heats the edge and makes the finish difficult to control.
Which sheets and films should be checked before laser processing?
You must know the composition of the sheet and of its protective film before any laser pass. PVC in particular is not recommended for this process.
What positioning accuracy does the Redline Mira 7 S offer?
The positioning accuracy specified for the Redline Mira 7 S is less than or equal to 0.1 mm. On the part, a glossy edge alone does not prove that the dimensions or straightness are compliant: check them separately.